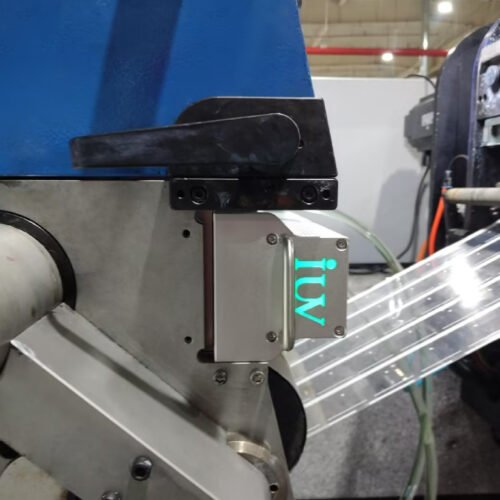
UV LED curing equipment is used in both digital and conventional label printing, but the requirements can differ significantly between the two processes. Digital presses may use dedicated UV-curable inks and require precise control during variable-data production. Conventional flexographic and offset presses often use different ink films, printing speeds and coating arrangements. In both cases, curing performance depends on the relationship between UV output, ink chemistry, substrate properties and production speed.
Choosing the right LED UV curing system requires more than comparing power ratings. The wavelength must suit the ink formulation, and the available UV energy must support the required production conditions. Poor matching can lead to weak adhesion, surface tack, reduced rub resistance or inconsistent finishing results.
This article explains how to match LED UV curing equipment to digital and conventional label printing. It covers ink compatibility, output settings, speed requirements, substrate considerations and practical testing methods. The focus is on helping OEMs, print businesses and engineers select and operate curing systems that deliver consistent results.
Introduction
Label printing includes several production methods, each with different curing requirements. Digital inkjet presses are widely used for short runs, variable data and frequent job changes. Conventional flexographic and offset presses remain important for longer runs and applications requiring specific print effects, high productivity or established production workflows.
UV LED curing can support both types of printing, provided the equipment is matched to the ink system and press design. However, a curing setup suitable for one process may not perform equally well on another. Digital inkjet inks, flexographic inks and offset inks can differ in viscosity, pigment content, film thickness and photoinitiator chemistry.
Production speed also affects the required curing conditions. A system must provide suitable UV exposure while the substrate moves through the curing area. Changes in speed, ink coverage or substrate type can alter the result.
The key is to treat the curing system, ink and printing press as one connected process. Equipment selection should begin with the actual printing requirements rather than a single power rating or a general assumption about LED UV performance.
1. Understanding the Differences Between Digital and Conventional Label Printing
Digital and conventional presses create printed images in different ways. These differences affect ink deposition, curing requirements and the way the curing system should be controlled.
In UV inkjet printing, the printheads deposit small droplets directly onto the substrate. The ink film can vary between image areas, depending on the design, colour coverage and printing settings. Some jobs contain large solid areas, while others use fine text, gradients or variable information.
The curing system must work with the inkjet press’s operating sequence. Depending on the machine design, UV exposure may occur shortly after ink deposition or at a later position along the web. The timing must allow the ink to cure without causing unwanted spreading or affecting the required image quality.
Conventional flexographic printing transfers ink through a plate, with the anilox roll controlling the amount of ink supplied. This can produce different ink-film thicknesses from those found in inkjet printing. Dense solids, white inks and high-coverage areas may place greater demands on the curing process.
Offset label printing has its own requirements, including ink transfer, ink formulation and the arrangement of printing units. The curing system must be compatible with the specific press and ink chemistry.
These differences explain why curing settings should not be transferred directly from one printing process to another. Each application requires its own validation.
2. Matching LED UV Wavelength to Ink Chemistry
Wavelength compatibility is one of the first factors to consider when selecting UV LED curing equipment. Common LED UV wavelengths include 365 nm, 385 nm and 395 nm. The suitable wavelength depends on the ink or coating formulation.
UV-curable inks contain photoinitiators that absorb UV radiation and initiate the curing reaction. If the LED wavelength does not match the photoinitiator system adequately, the ink may not cure properly even when the system operates at a high output setting.
This is particularly important when changing from conventional mercury UV curing to LED UV curing. A conventional UV ink may not be suitable for an LED system unless its formulation is designed to respond to the available wavelength.
Digital inkjet inks should be checked against the press manufacturer’s approved ink specifications. Conventional flexographic and offset inks also require confirmation of wavelength compatibility. The fact that two inks are both described as UV-curable does not mean they will respond identically to the same LED source.
Pigments can further influence curing. White and heavily pigmented inks may limit how much UV radiation reaches deeper parts of the ink film. Clear varnishes may behave differently because their optical properties and formulations are not the same.
Before selecting equipment, confirm the intended wavelength with the ink supplier. This simple step can prevent unnecessary adjustments and reduce the risk of selecting a curing system that cannot meet the application’s requirements.
3. Matching UV Output to Ink Film Thickness and Coverage
The amount of ink deposited on the substrate affects the curing process. Thicker ink films generally require careful evaluation because UV radiation must reach the reactive components throughout the printed layer.
In digital printing, ink coverage can vary considerably across a label design. A job with small text and light graphics may behave differently from one containing large solid areas or multiple overlapping colours.
In flexographic printing, the anilox roll, ink condition and printing settings influence the deposited ink film. If the ink transfer is higher than intended, the curing system may struggle to maintain the required performance at the same production speed.
Offset printing also requires attention to the actual ink film and the characteristics of the ink formulation. A curing setting developed for one ink or print configuration should not automatically be assumed suitable for another.
When curing problems occur, check both the UV output and the amount of ink deposited. Increasing output may help when the ink receives insufficient UV energy, but it will not necessarily solve problems caused by an unsuitable formulation or excessive ink transfer.
A practical approach is to test representative designs and colour combinations. Include high-coverage areas, opaque colours and any coatings used in the final product. This helps establish a reliable operating range for the actual job.
4. Setting UV Output According to Print Speed
Print speed determines how long the substrate remains under the curing head. When a press runs faster, the ink receives UV radiation for a shorter period.
If the output remains unchanged, the available UV energy may become insufficient for the ink and production conditions. This can lead to poor adhesion, reduced rub resistance or other signs of incomplete curing.
The correct response depends on the press and curing system. Some systems allow the output to be adjusted automatically according to line speed. Others require operators to select or confirm settings for different production conditions.
For digital label presses, the curing system must follow the machine’s operating sequence and permitted speed range. Job changes and transitions between printing modes may require different validated settings.
For conventional presses, the system should be checked at the intended production speed, including any normal acceleration and deceleration. Testing only at a low speed may not reveal problems that occur during full production.
Engineers should begin with the ink supplier’s recommendations and the equipment manufacturer’s operating limits. They can then run controlled trials at different speeds and check whether the printed ink meets the agreed quality requirements.
The aim is not to use the highest possible UV output. It is to provide enough suitable UV energy for reliable curing without operating the equipment outside its intended range.
5. Understanding Irradiance and Overall Curing Performance
Irradiance describes the UV power reaching a surface at a particular moment. It is commonly measured in watts per square centimetre or milliwatts per square centimetre. The total UV energy received during exposure also matters.
A high irradiance reading does not automatically prove that the ink is fully cured. The wavelength, ink chemistry, exposure conditions and ink-film thickness all influence the result.
Two LED UV systems may show similar readings but perform differently with a particular ink. Their wavelength characteristics, output distribution and operating conditions may differ.
Measurements should therefore be taken at a relevant position, ideally representing the actual substrate plane. The instrument must be suitable for the wavelength being measured, and the test conditions should be recorded.
For digital and conventional label printing, curing performance should be confirmed using the ink supplier’s recommended evaluation methods. Depending on the application, these may include adhesion, rub resistance, scratch resistance and checks after downstream converting.
This approach connects equipment measurements with actual print quality. It also helps engineers determine whether a problem comes from the curing system or another part of the printing process.
6. Choosing the Right System for Paper and Film Substrates
Label presses may run paper, coated paper, polypropylene, polyethylene, polyester and other flexible materials. These substrates differ in surface properties, thickness and heat sensitivity.
An ink that cures well on paper may not provide the same adhesion on a plastic film. Some films require suitable surface treatment to achieve reliable ink bonding. Contamination can also affect adhesion.
LED UV curing equipment can reduce some heat transfer compared with many conventional UV configurations. However, it still generates heat, and the substrate can absorb energy during curing.
Thin films require particular attention because temperature changes may affect dimensional stability. Shrinkage or stretching can influence registration, die-cutting accuracy and label appearance.
When selecting a curing system, consider the full range of materials used in production. Testing should include the most heat-sensitive substrates and the jobs with the highest curing demands.
If adhesion problems occur, check the substrate and ink compatibility before increasing UV output. Additional energy cannot correct every surface-related issue.
7. Managing Print Quality and Registration
Consistent curing supports stable print quality, but registration problems may have several causes. The curing process is only one part of the overall press operation.
In digital printing, changes in web movement or substrate dimensions can affect the position of printed images. In conventional printing, mechanical settings, web tension and plate or cylinder conditions can also influence registration.
If registration changes during production, engineers should check the press speed, web tension and substrate condition. They should also examine whether the defect coincides with changes in curing output or material temperature.
Excessive heat may contribute to dimensional changes in sensitive films. However, reducing UV output without confirming adequate curing can create a different quality problem.
A controlled test can help separate these issues. Compare registration and substrate condition at several approved operating speeds while checking ink curing performance. This makes it easier to identify whether the cause is mechanical, thermal or related to the curing process.
Stable press operation and suitable curing settings should be established together rather than adjusted independently.
8. Avoiding Surface Tack and Incomplete Curing
Surface tack is a common reason for investigating UV curing performance. It may indicate insufficient curing, but the underlying cause is not always a lack of output.
Some UV-curable inks and coatings are affected by oxygen inhibition. Oxygen can interfere with the curing reaction at the exposed surface, leaving a tacky layer even when the material beneath it has cured more effectively.
The first step is to confirm the ink’s suitability for the selected LED wavelength. Check the output settings and ensure that the system is operating correctly. If the problem continues, consult the ink supplier about the formulation and recommended curing conditions.
Testing should include the properties that matter for the final label. A dry-looking surface may still have poor adhesion or rub resistance. Conversely, surface tack may be linked to formulation or surface effects rather than insufficient curing throughout the film.
For applications with demanding performance requirements, use documented acceptance criteria. This helps the production team make adjustments based on test results rather than appearance alone.
9. Low-Migration Requirements for Label Applications
Some labels are used on packaging where migration of ink components must be carefully controlled. Food packaging is one example, although the specific requirements depend on the product, packaging construction and intended use.
In these applications, adequate curing is important, but curing alone does not guarantee compliance with applicable migration requirements. Ink formulation, photoinitiator selection, substrate properties, printed layer thickness and the overall packaging design all matter.
The printer should use an ink system intended for the relevant application and follow the supplier’s technical guidance. The curing process must also be validated under representative production conditions.
Digital and conventional presses may use different ink formulations, so their curing settings and validation records should be assessed separately. A setting that produces acceptable rub resistance does not, by itself, demonstrate that migration requirements have been met.
Where low-migration performance is required, work with the ink supplier and packaging technical team to establish the necessary controls and verification procedures. Avoid relying on general UV output settings as a substitute for application-specific assessment.
10. Integrating LED UV Equipment into Existing Presses
When retrofitting LED UV curing equipment, engineers should review the mechanical, electrical and control requirements before installation.
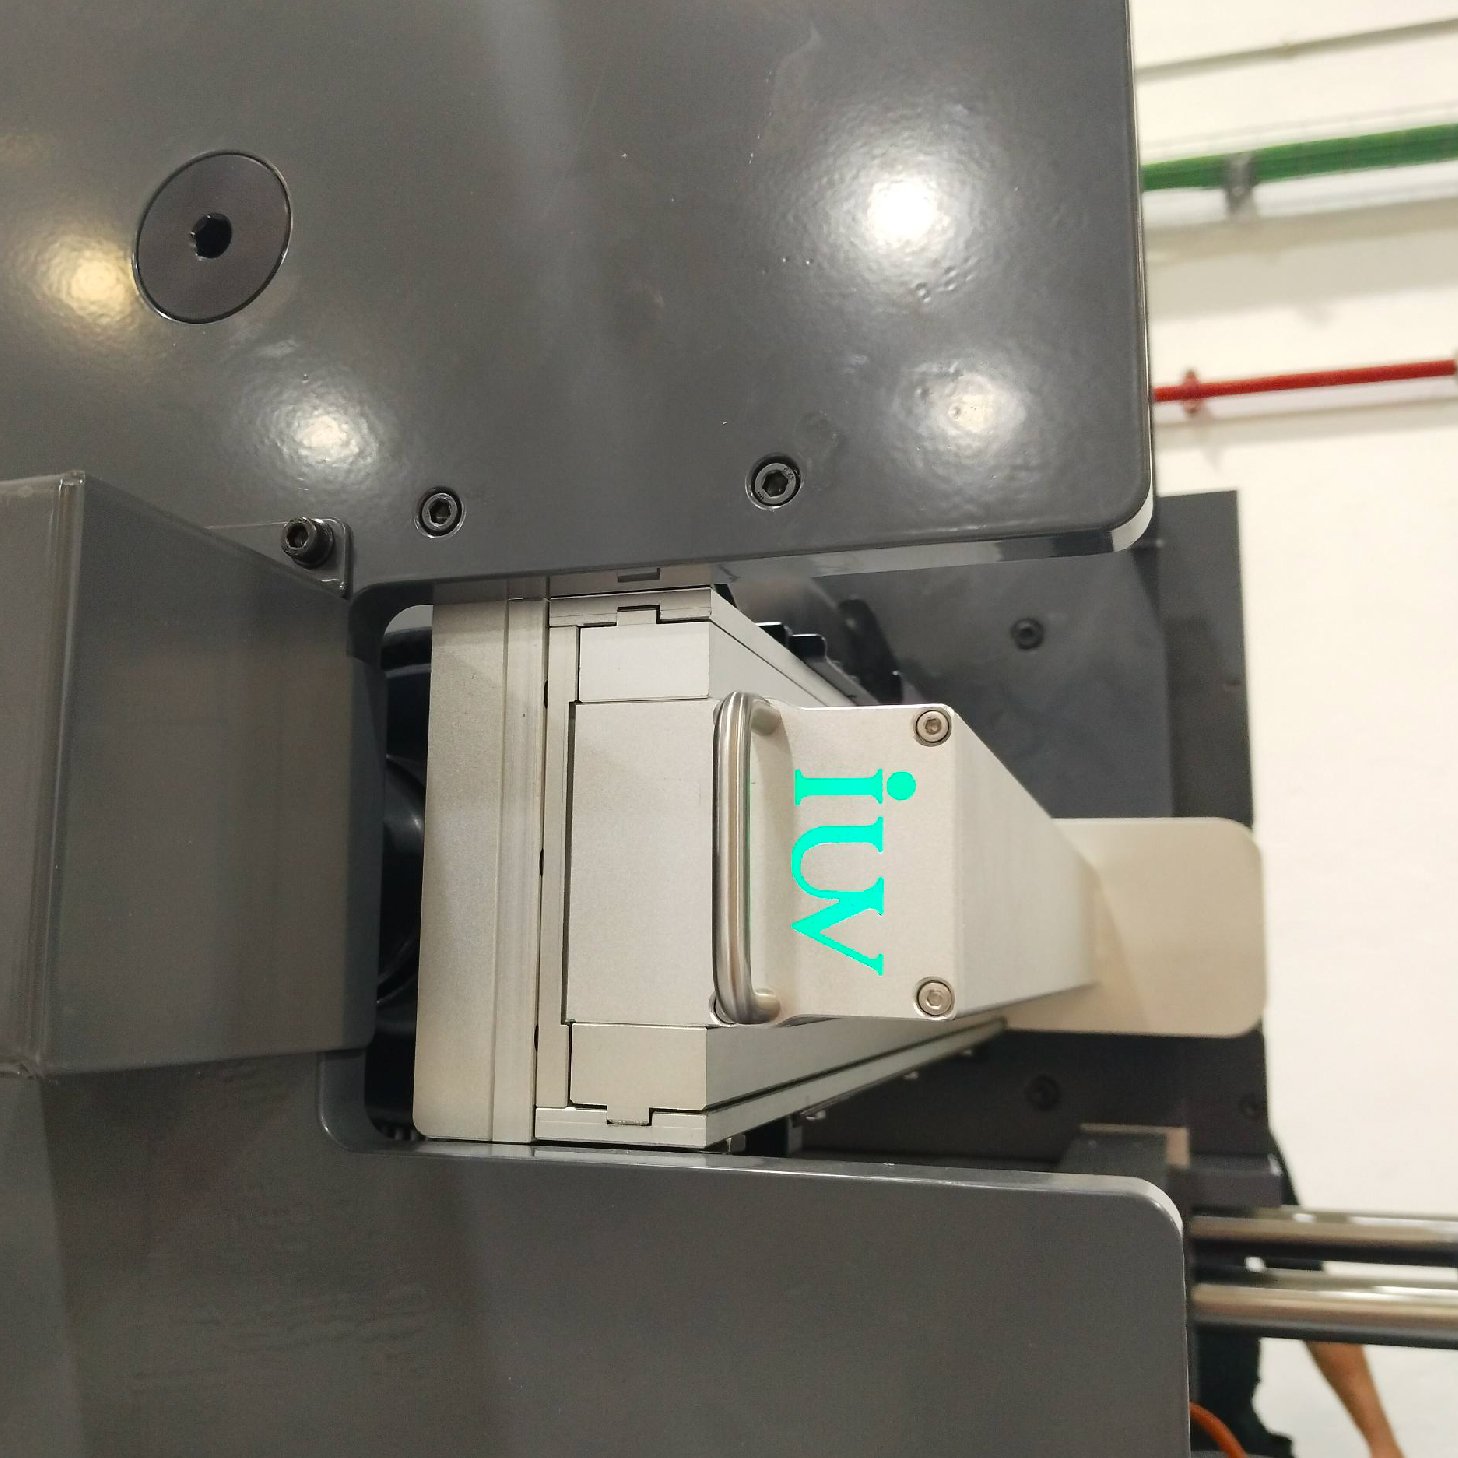
The available space must accommodate the curing head, mounting hardware, cables and cooling connections. The installation should allow access for cleaning and maintenance while maintaining the required distance and alignment between the curing head and substrate.
Electrical checks should cover the power supply, protective devices, grounding and compatibility with the press control system. The curing controller must receive the correct operating signals and respond appropriately to speed changes.
Cooling capacity is another important factor. Water-cooled systems require suitable flow and inlet temperature, while the cooling arrangement must support the intended production conditions.
The control sequence should account for press stops, communication faults and cooling alarms. These conditions should be tested before the system enters routine production.
A retrofit assessment should also confirm that the selected system can meet the requirements of the intended inks, substrates and production speeds. This reduces the risk of installing equipment that fits mechanically but cannot deliver the required curing performance.
11. Commissioning and Troubleshooting
Commissioning should begin with checks of the installation, electrical connections, cooling system and safety functions. Engineers should then confirm the LED wavelength and establish initial settings based on the ink supplier’s recommendations.
Run representative jobs at a manageable speed and inspect the results. Increase the speed in controlled steps, recording the output setting and curing performance at each stage.
Include jobs that represent the most demanding conditions. These may involve dense colours, white ink, heavy ink coverage, multiple layers or heat-sensitive films.
If undercuring occurs, investigate the possible causes in a logical order:
- Confirm that the ink is compatible with the LED wavelength.
- Check the UV output and measurement conditions.
- Verify that the press speed is within the validated operating range.
- Review ink-film thickness and printing settings.
- Inspect the curing head and cooling system.
- Check substrate compatibility and surface treatment.
- Repeat the relevant curing tests after making an adjustment.
Only change one major variable at a time wherever practical. This makes the result easier to interpret and helps prevent unnecessary changes to other press settings.
After successful testing, document the approved conditions for each representative job. Repeat validation when a significant change in ink, substrate or production conditions may affect curing performance.
12. Maintaining Consistent LED UV Performance
LED UV curing equipment needs regular inspection to maintain stable output. Dust, ink mist and coating residue can accumulate around the curing head and affect the UV energy reaching the printed material.
Clean optical surfaces according to the equipment manufacturer’s instructions. Use suitable materials and avoid damaging the components.
For water-cooled systems, check coolant flow, inlet temperature and possible leaks. Inspect electrical connections and cables for damage or signs of overheating.
Periodic irradiance measurements can help identify changes in performance. Use a suitable instrument and repeat measurements under comparable conditions so that results can be compared with the original commissioning records.
Production records should include the ink type, substrate, press speed, output settings and relevant test results. These records help engineers identify whether a change in curing performance is associated with equipment condition, materials or production settings.
Regular maintenance and documented operating conditions make it easier to keep digital and conventional label printing processes consistent over time.
Conclusion
UV LED curing equipment for digital and conventional label printing must be matched to the ink chemistry, print speed and substrate. Although both printing methods can use LED UV curing, their ink deposition, operating sequences and production requirements may differ.
Correct wavelength selection is the starting point. Irradiance and speed settings must then be validated with the actual ink and substrate, while ink-film thickness, heat sensitivity and surface properties should also be considered.
For OEMs and end users, a practical approach combines equipment assessment, controlled production trials and regular maintenance. Documented curing tests help confirm that the selected settings remain suitable when jobs or operating conditions change.
By treating the press, ink and curing system as one connected process, printers can reduce curing defects and maintain consistent label quality across digital and conventional production.