Abstract
Sheetfed offset production increasingly combines conventional UV offset inks, LED UV inks, hybrid formulations, coatings, and specialty substrates on the same press. In these jobs, curing performance depends not only on lamp power. The sequence, wavelength, irradiance, exposure position, ink film thickness, coating load, and substrate heat tolerance must work as one process. A UV curing system that performs well on a full-LED job may behave differently when conventional hybrid ink is followed by an LED-curable coating or when a heavy coating layer is applied after several ink units.
Lamp sequence therefore becomes an engineering parameter rather than a simple machine configuration. The correct sequence can improve interstation cure, reduce set-off, stabilize trapping, and maintain surface quality without adding unnecessary thermal load. This article examines how sheetfed offset printers and OEM engineers can tune UV curing systems for hybrid ink and coating applications, with particular attention to wavelength matching, irradiance, curing energy, oxygen inhibition, heat management, and practical troubleshooting.
Introduction
The search intent behind “UV curing systems for sheetfed offset” is primarily technical and commercial investigation. Press owners want to understand how a UV system will behave on real production jobs, while OEMs and engineers need practical criteria for integrating curing modules into a press architecture. For hybrid ink and coating production, the key question is not simply whether a lamp can cure an ink. The more important question is where, when, and with how much UV energy the material should be cured.
Sheetfed offset differs from many narrow-web applications because the process can involve relatively high ink coverage, fine screens, solid areas, coating units, variable sheet sizes, and substrates with different thermal characteristics. Hybrid ink systems also create a process in which conventional and UV-reactive chemistry may coexist. The curing system must provide enough energy to develop the required film properties while avoiding excessive heat, premature surface cure, or unnecessary exposure to later coating layers.
A useful approach is to treat the press as a sequence of material transformations. Each print unit changes the surface condition of the sheet. Each curing stage then changes the mechanical and chemical condition of the ink film before the next unit receives the sheet. Lamp sequence should therefore be tuned according to the job structure rather than selected independently from the ink and coating system.
Understanding Lamp Sequence in Sheetfed Offset
In a sheetfed offset press, UV curing modules may be installed between selected printing units, near the delivery section, or in combinations that provide both intermediate and final curing. The required configuration depends on the ink system, coating chemistry, press speed, coverage, substrate, and finishing requirements.
For a hybrid ink job, an early curing station can be used to increase ink film stability before subsequent printing or coating operations. A later station can provide additional energy for through-cure and surface cure. This does not mean that every unit needs maximum UV output. Excessive intermediate curing can change the surface properties of the ink film and influence subsequent ink transfer, trapping, or coating wetting.
The engineering objective is to establish a sufficient cure window at each stage. The first exposure should stabilize the printed film enough for the next process step. The final exposure should deliver the required cure depth and surface properties. Between these points, the UV dose should be distributed according to the actual job rather than concentrated automatically at one location.
Lamp sequence also affects maintenance. When the curing load is distributed across multiple modules, individual units may operate below their maximum capacity. This can provide more flexibility when production changes from light coverage to heavy solids or from hybrid inks to UV coatings.
LED UV Wavelength and Photoinitiator Matching
LED UV curing systems normally operate at defined wavelength bands, commonly around 365, 385, 395, or 405 nm. The appropriate wavelength is determined by the absorption characteristics of the photoinitiator package used in the ink or coating.
A higher irradiance does not automatically compensate for poor spectral matching. If the formulation does not efficiently absorb the available wavelength, increasing electrical power can produce additional heat without delivering proportional curing improvement. For this reason, the first engineering check should be compatibility between the LED emission spectrum and the ink or coating formulation.
Hybrid ink requires particular attention because its curing mechanism may differ from a dedicated LED UV formulation. The ink supplier should confirm the recommended wavelength and curing window. The same principle applies to UV coating. A coating with a different photoinitiator package may require a different exposure condition from the ink underneath it.
For an OEM integration project, the wavelength should therefore be considered at the system-design stage. The curing module, optical configuration, ink chemistry, coating chemistry, and production speed should be evaluated together. Changing only the lamp while keeping all other parameters constant can lead to an unstable process window.
Irradiance, UV Dose, and Press Speed
UV curing performance is governed by both irradiance and exposure time. Irradiance describes the UV power received by the printed surface, while UV dose represents the accumulated energy delivered during exposure. In simplified terms, increasing press speed reduces exposure time and therefore reduces dose when other conditions remain unchanged.
This relationship becomes important when tuning lamp sequence. A high-power final lamp may compensate for a demanding coating layer, while a lower-power intermediate module may be sufficient for stabilizing an ink film. The correct setting should be verified with production tests rather than selected from lamp power alone.
UV dose should also be considered together with ink film thickness. Heavy solids, dense process colors, opaque inks, and coatings can require more curing energy than thin films. The optical path through the printed layer becomes more demanding as coverage increases. A setting that works on a light screen may therefore fail on a large solid area.
A practical production trial should record press speed, lamp output, measured irradiance, estimated or measured UV dose, ink type, coating type, substrate, and print coverage. Comparing these variables makes it easier to distinguish a curing problem from an ink-transfer or coating problem.
Lamp Sequence for Hybrid Ink and Coating Jobs
A common hybrid workflow may print several ink units, apply a coating, and then perform final UV curing. In such a configuration, the curing sequence should be designed around the physical condition of the ink film at each point.
If intermediate curing occurs too early or at excessive intensity, the surface can become less receptive to the next ink or coating layer. If curing is insufficient, the film may remain mechanically unstable and create set-off or surface defects later in the press. The useful range lies between these conditions.
For example, an intermediate LED UV module can be configured to provide controlled stabilization after selected ink units. The final curing station can then provide the higher dose required for the complete ink and coating stack. This approach is particularly useful when the coating is applied over a substantial ink film and the final surface must resist blocking, scratching, or handling damage.
The sequence should also reflect the coating position. A coating applied before a final curing station may need a different exposure strategy from a coating that receives a dedicated curing module immediately after application. Coating thickness, transparency, pigment concentration, and surface requirements all influence the result.
Ink Film Thickness, Coverage, and Offset Stability
Offset ink transfer creates a variable film thickness across the sheet. Fine text and halftone areas may contain relatively thin films, while solids can carry substantially more material. A curing system must therefore handle the highest practical load without over-curing the lighter areas.
Heavy ink coverage can produce several symptoms when curing capacity is insufficient. The printed sheet may show set-off during stacking, poor scratch resistance, residual odor, incomplete surface cure, or weak resistance during subsequent finishing. These symptoms can become more apparent when press speed increases.
Conversely, excessive UV exposure can create a surface that cures rapidly while the lower part of the film remains less developed. This can be especially relevant for thick or highly pigmented films. Engineers should therefore evaluate both surface cure and overall film performance rather than judging the result only by touch.
Job-specific testing should include representative solids, fine screens, small text, and the actual coating structure. A curing setting validated only on a test image may not represent the highest material load encountered in production.
Oxygen Inhibition and Surface Cure
Oxygen inhibition is a critical factor in UV-curable systems. Oxygen at the surface can interfere with free-radical polymerization and leave the uppermost layer insufficiently cured. The effect can become more visible at low UV dose, high press speed, thin films, or formulations with limited surface-curing capability.
When a sheet shows a soft or slightly tacky surface despite apparently adequate lamp output, oxygen inhibition should be considered alongside wavelength compatibility and dose. Increasing irradiance may improve the situation, but it should not be the only adjustment.
The formulation itself is important. Photoinitiator concentration, reactive monomers, oligomers, additives, and surface chemistry influence the response to UV exposure. Therefore, the curing system and ink formulation must be treated as a matched process.
For hybrid ink and coating jobs, surface cure should be checked after the complete curing sequence. A coating may change the oxygen exposure and optical behavior of the underlying ink film. The final result can therefore differ from the cure behavior of the ink before coating.
Thermal Management for Sensitive Substrates
Sheetfed offset applications include substrates with different thermal limits. Lightweight papers, synthetic sheets, plastic-based media, films, and specialty stocks can respond differently to heat generated by UV systems.
LED UV technology can reduce unnecessary infrared heat compared with some conventional UV configurations, but the complete curing module still produces thermal energy. The substrate receives heat from the LED array, optical components, surrounding press structures, and the printed film itself.
Water cooling is commonly used in higher-output LED UV systems to stabilize LED operating temperature and maintain consistent optical performance. Thermal management should also consider airflow, heat transfer through the press frame, substrate temperature, and the distance between the curing window and sheet surface.
A useful production test should measure substrate behavior at the actual production speed. Curling, dimensional change, coating distortion, substrate deformation, and changes in surface appearance may appear only after sustained operation.
Low-Migration Considerations
Packaging applications may require low-migration ink and coating systems. In such applications, curing is part of the overall migration-control strategy, but lamp settings alone cannot establish compliance.
The ink and coating supplier should specify the applicable curing conditions and recommend the compatible photoinitiator system. The press should then reproduce these conditions consistently. Insufficient curing can leave residual reactive components, while excessive exposure may create other process or substrate effects.
For low-migration work, process control is particularly important. Lamp output should be monitored, curing windows should be kept consistent, and changes in press speed or material coverage should be documented. Any validation should be performed against the applicable packaging requirements and the specific formulation being used.
Troubleshooting Common Curing Defects
When a sheet shows incomplete cure, the troubleshooting sequence should begin with basic process data. Confirm the actual press speed, LED output, irradiance at the substrate plane, lamp-to-sheet distance, wavelength, and cooling condition. Then check the ink and coating batch specifications.
If the surface remains tacky, first distinguish oxygen inhibition from insufficient total dose. If the problem occurs mainly in heavy solids, investigate dose distribution, ink film thickness, and spectral absorption. If only one color or coating shows the problem, formulation compatibility should be checked before increasing the output of every curing module.
Set-off in the delivery pile can have several causes. Insufficient curing is one possibility, but excessive ink film, inappropriate powder settings, substrate characteristics, or coating behavior can also contribute. Increasing UV power without identifying the actual cause may increase heat while leaving the underlying process problem unresolved.
Poor trapping or unstable overprinting after an intermediate lamp can indicate excessive early curing. In that case, reducing the intermediate exposure may restore the required surface interaction between layers. The final curing station can then provide the remaining dose required for the finished structure.
Retrofit Conditions for Existing Sheetfed Presses
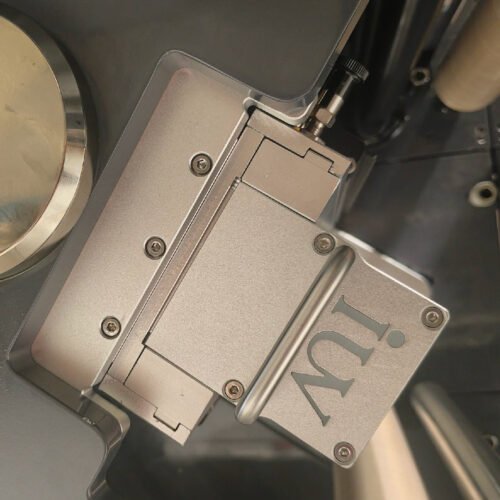
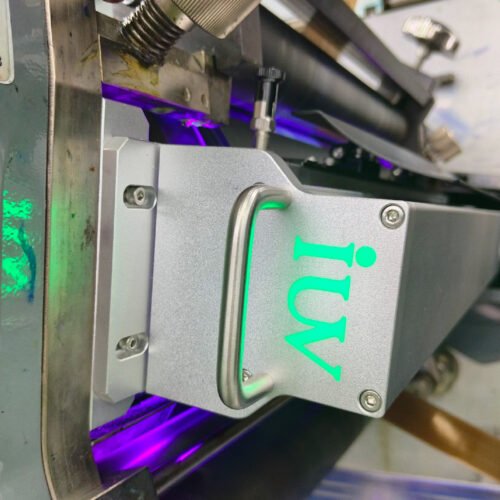
Retrofitting an LED UV curing system onto an existing sheetfed press requires more than confirming available electrical power. The mechanical envelope, sheet path, lamp-to-sheet distance, cooling infrastructure, exhaust arrangement, control interface, safety interlocks, and available installation space must all be checked.
The position of the existing UV module is particularly important. A retrofit that places the LED array too far from the sheet can reduce irradiance at the substrate. A poorly selected installation position can also create an unsuitable angle or interfere with downstream equipment.
Press control integration should allow operators to reproduce validated curing conditions. Depending on the system architecture, this may include lamp power adjustment, cooling monitoring, interlocks, fault signals, and production-speed coordination.
A retrofit should also be evaluated against the customer’s actual job mix. A system intended mainly for hybrid ink may need a different curing distribution from one intended for heavy UV coating. The engineering specification should therefore begin with representative production samples rather than a generic lamp rating.
Maintenance and Output Stability
LED UV systems do not require lamp replacement in the same way as conventional mercury UV systems, but they still require routine maintenance. Optical windows can accumulate ink mist, coating residue, dust, and paper debris. Contamination reduces the amount of UV reaching the substrate.
Cooling performance is equally important. Restricted water flow, incorrect coolant conditions, blocked heat exchangers, or abnormal temperatures can affect system stability. Regular inspection should include cooling parameters, optical surfaces, electrical connections, and safety interlocks.
Output verification should be performed at defined intervals. A curing system that produces acceptable results immediately after installation may require recalibration or cleaning after extended production. Consistent monitoring is especially important for packaging and high-value commercial print, where small changes in cure can affect downstream finishing.
A Practical Tuning Procedure
Lamp sequence should be tuned through controlled production trials. Start with the ink and coating supplier’s recommended wavelength and curing range. Establish a baseline at the normal production speed using representative substrate and coverage.
Next, evaluate the intermediate curing station independently. The target is sufficient film stabilization without unnecessarily changing the surface condition before the next printing or coating unit. Then evaluate the final curing station with the complete ink and coating stack.
Record defects by location and coverage. If the problem appears only after a specific unit, examine the curing condition immediately before that unit. If the entire sheet shows weak final cure, examine the final station, total dose, spectral compatibility, and cooling condition.
Once a stable window has been identified, document the settings for typical job classes. Separate settings may be appropriate for light coverage, heavy solids, hybrid ink with coating, and specialty substrates. This provides operators with repeatable production parameters instead of relying on subjective adjustments.
Conclusion
For sheetfed offset production, UV curing is a process-control problem rather than a simple lamp-power problem. Hybrid ink and coating jobs require careful coordination between wavelength, irradiance, UV dose, ink film thickness, press speed, lamp position, and thermal management.
A well-defined lamp sequence can stabilize intermediate ink films while reserving sufficient curing capacity for the final ink and coating structure. The correct balance depends on the formulation and job conditions. Excessive intermediate exposure can affect subsequent printability, while insufficient exposure can lead to set-off, poor surface cure, and finishing problems.
For OEMs and press users, the most reliable approach is to define the curing system around actual production requirements. Representative substrates, ink coverage, coating loads, press speeds, and required surface properties should be included in validation trials. Once these variables are measured and documented, LED UV curing becomes a controllable part of the sheetfed offset process rather than an isolated equipment parameter.